
Dimensions held in the morning can drift in the afternoon
If the ballbar is good when cold but deviates after the machine warms up, the frame cannot compensate for thermal expansion. Rigid casting and cooled drives help here.
Request a quote. The Art of Milling — Wiesser Precision Europe. Unclamping and reclamping a part leads to dimensional inaccuracies. Finishing the job in a single setup reduces both scrap and downtime.
Machine selection
The right machine is determined by the number of setups, material, and tolerance before the table, spindle, and axes.
If the ballbar is good when cold but deviates after the machine warms up, the frame cannot compensate for thermal expansion. Rigid casting and cooled drives help here.
Clamping the part a second time introduces zero shift and angular deviation. For multi-sided jobs, 5-axis makes it possible to finish in a single setup.
If spindle rigidity and axis stability are insufficient, chatter begins, tool life decreases, and dimensional accuracy is lost. Sound and chip formation indicate this immediately.

Seen on the shop floor
When proper cooling, sufficient spindle torque, and stable axis movement are combined, surface finish is maintained, and dimensions are held throughout the shift. Otherwise, scrap increases.
View CNC machines →CNC Machines
Lathe for shafts and flanges; vertical machining for prismatic bodies; 5-axis for multi-sided parts; bridge type for large molds. 156 models, 8 machine types.

Do not unclamp and reclamp multi-sided parts. Zero shift is one of the most common causes of scrap.
5-Axis Models →
When machining titanium, nickel, and hard steel, heat transfers to the machine frame. If thermal compensation is poor, dimensional deviations occur between the start and end of the part.
Read Why →Industries
In aerospace and defense, an out-of-tolerance part is scrap. In automotive and mold making, cycle time and surface quality stand out.

Wing mount, landing gear, engine bracket.
Explore the industry
Engine, transmission, and brake components.
Explore the industry
Injection molds, stamping and sheet metal dies.
Explore the industry
Tight tolerances, rigid frame, hard alloys.
Explore the industry
Turbine shaft, valve body.
Explore the industry
Structural components, single-setup machining.
Explore the industryFeatured Models
Flagship models selected based on table size, spindle type, and clamping requirements.
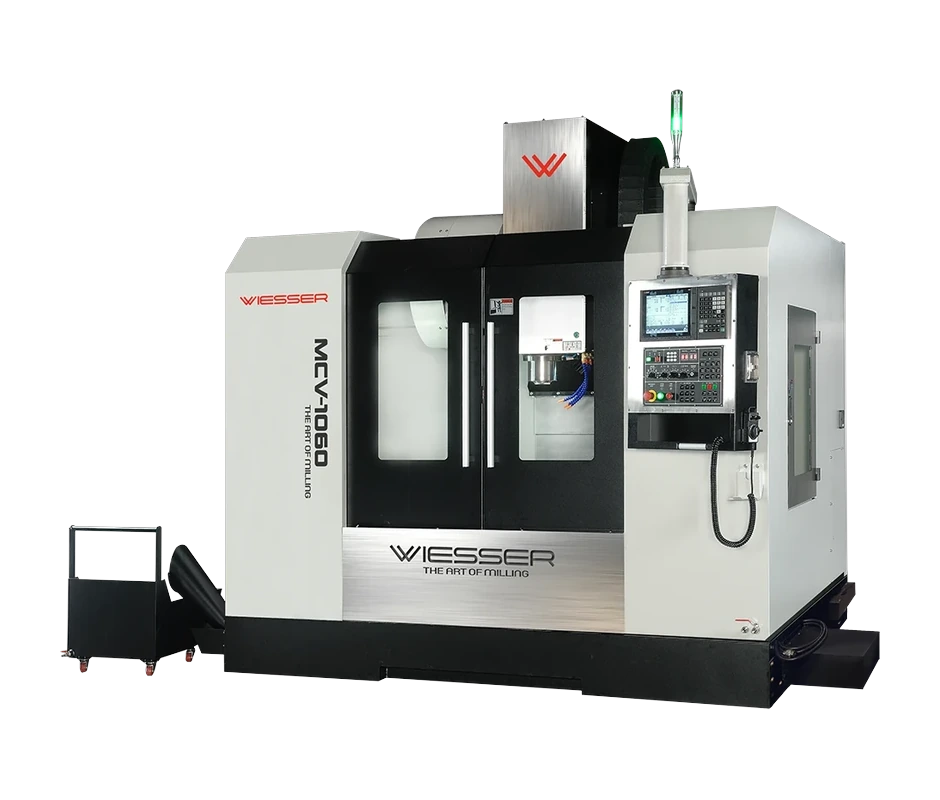
Table 1,100 × 600 mm · Medium housing and mold work
Specs →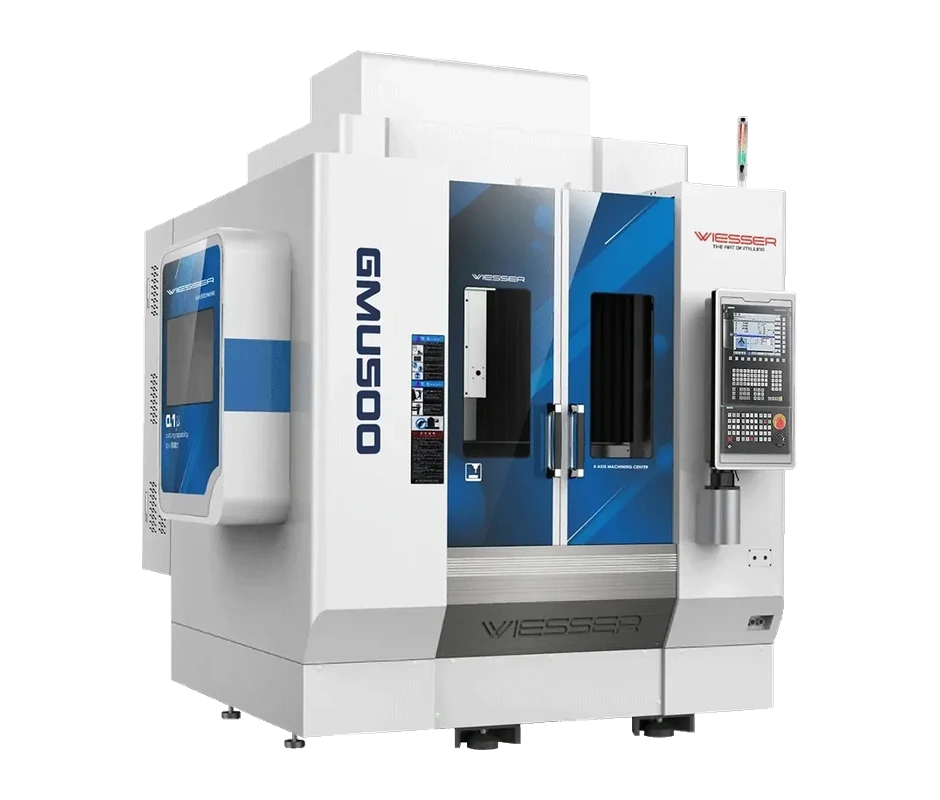
Table Ø500 · A/C rotary axis · Multi-face machining in a single setup
Specs →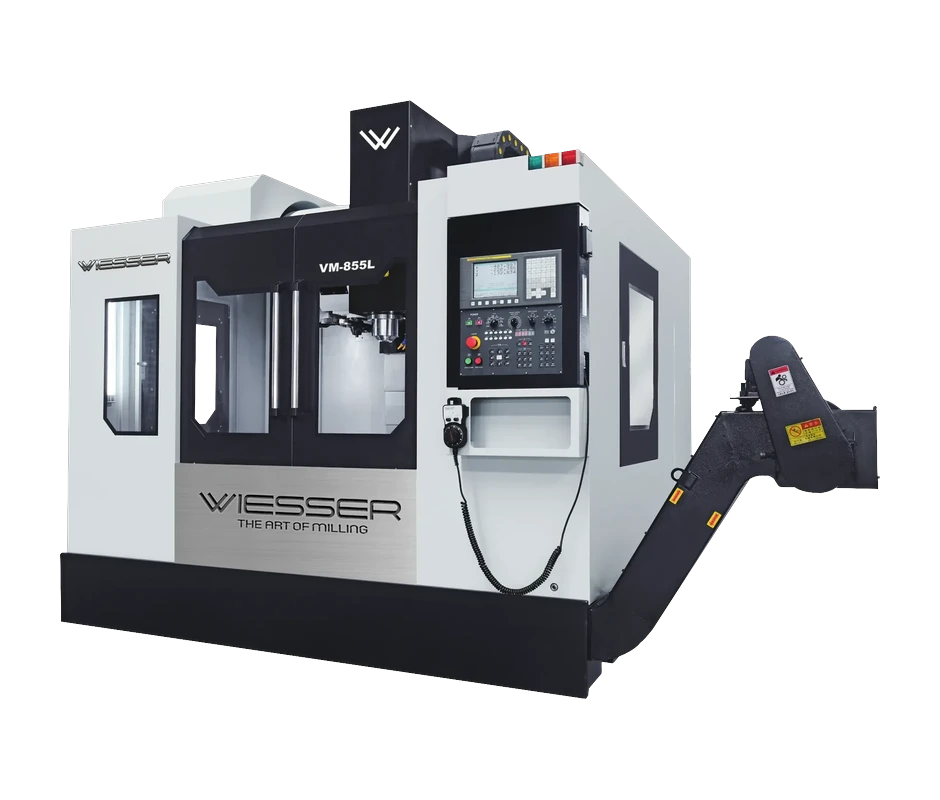
Direct drive spindle · Serial prismatic parts
Specs →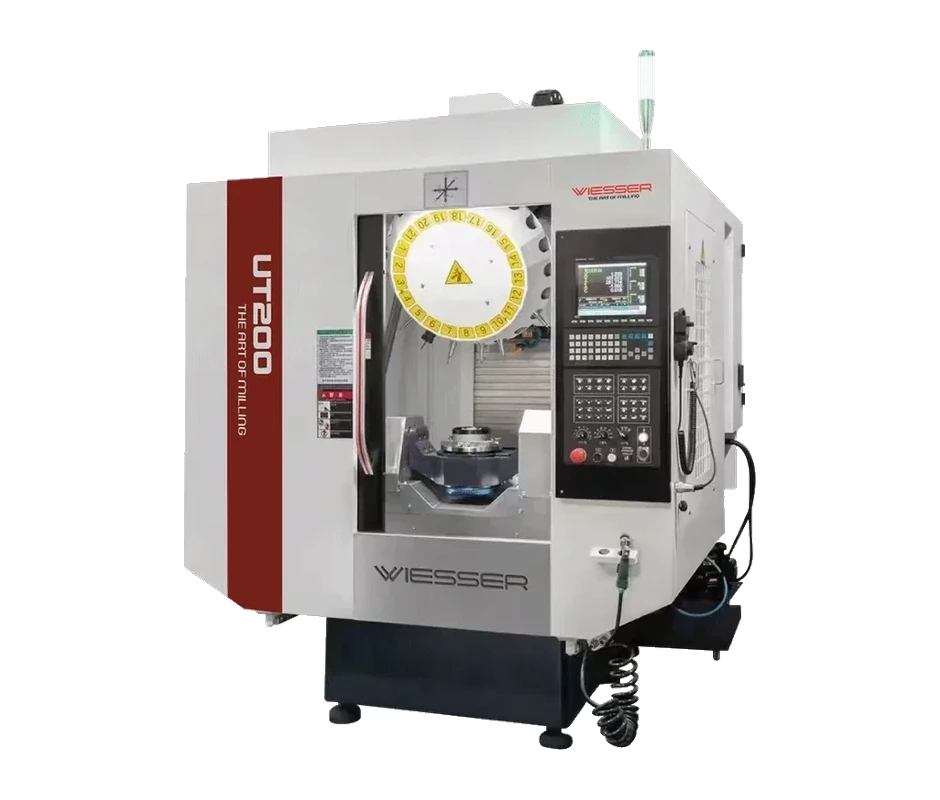
Table Ø260 · 20,000 rpm · Small precision parts
Specs →Technical Service
Not only during breakdowns; we reduce production downtime with calibration, spindle, and CAM support.
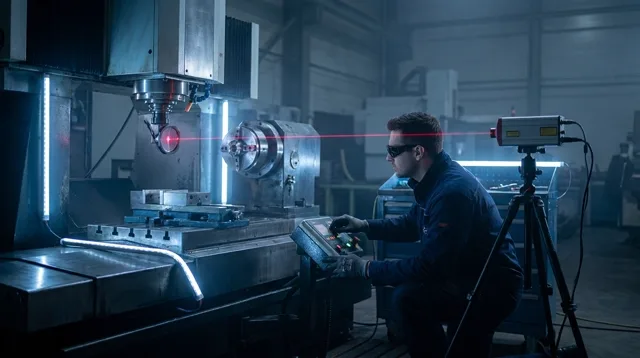 01
We catch axis backlash and geometry deviation before scrap. Periodic calibration prevents dimensional inaccuracies.
 02
Spindle, drive, or encoder? We find the source through measurement; diagnosis first, then the part.
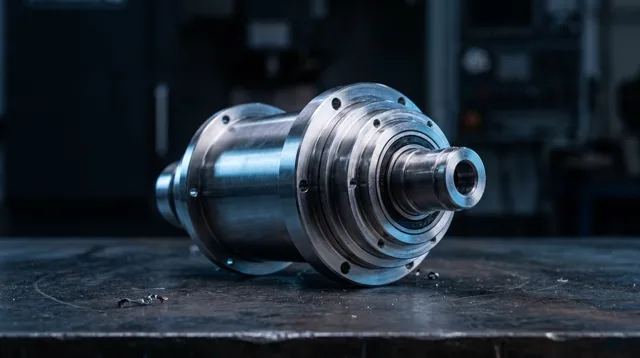 03
Aftermarket bearings or screws compromise rigidity. OEM specifications maintain the stated repeatability.
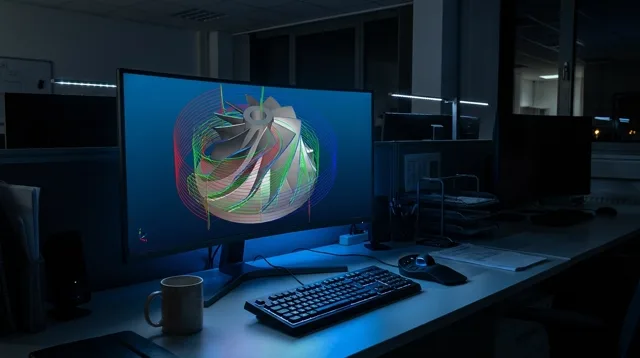 04
By optimizing toolpaths and cutting parameters, we reduce idle time on the same machine.
Machine Finder
Select one of the types below; the product list will open with that filter.
Blog
CNC Lathe selection, ballbar calibration, spindle failure, control unit, and CAM — 21 articles, a constantly expanding archive.
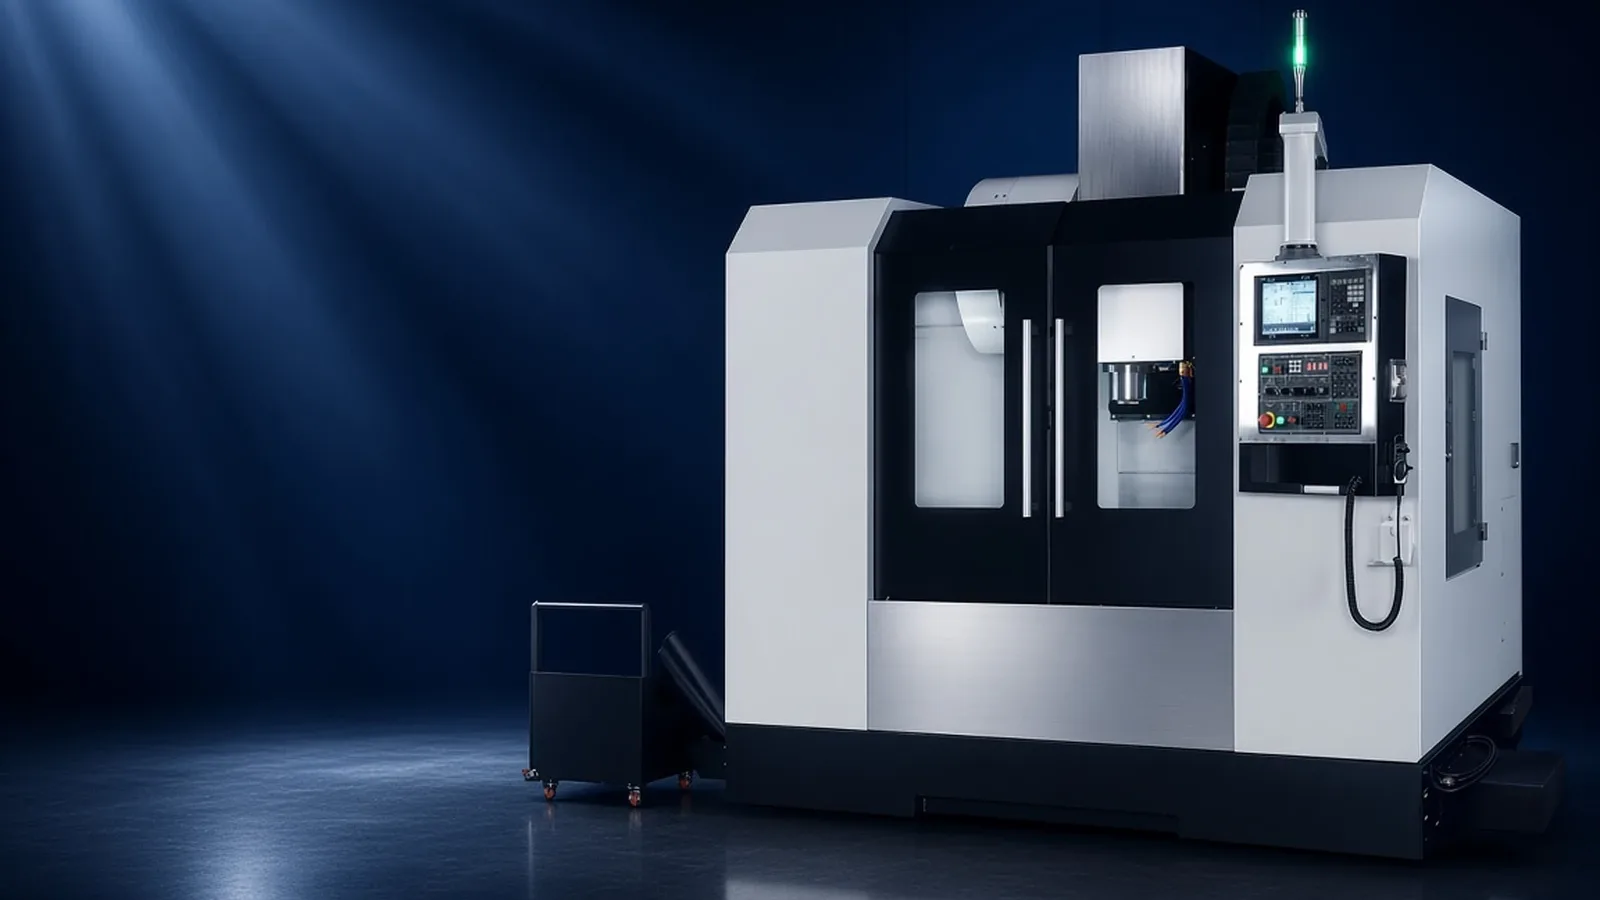
Part form, tolerance, clamping, and control unit — pre-investment checklist.
Lathe capacity based on shaft, flange, and live tooling requirements.
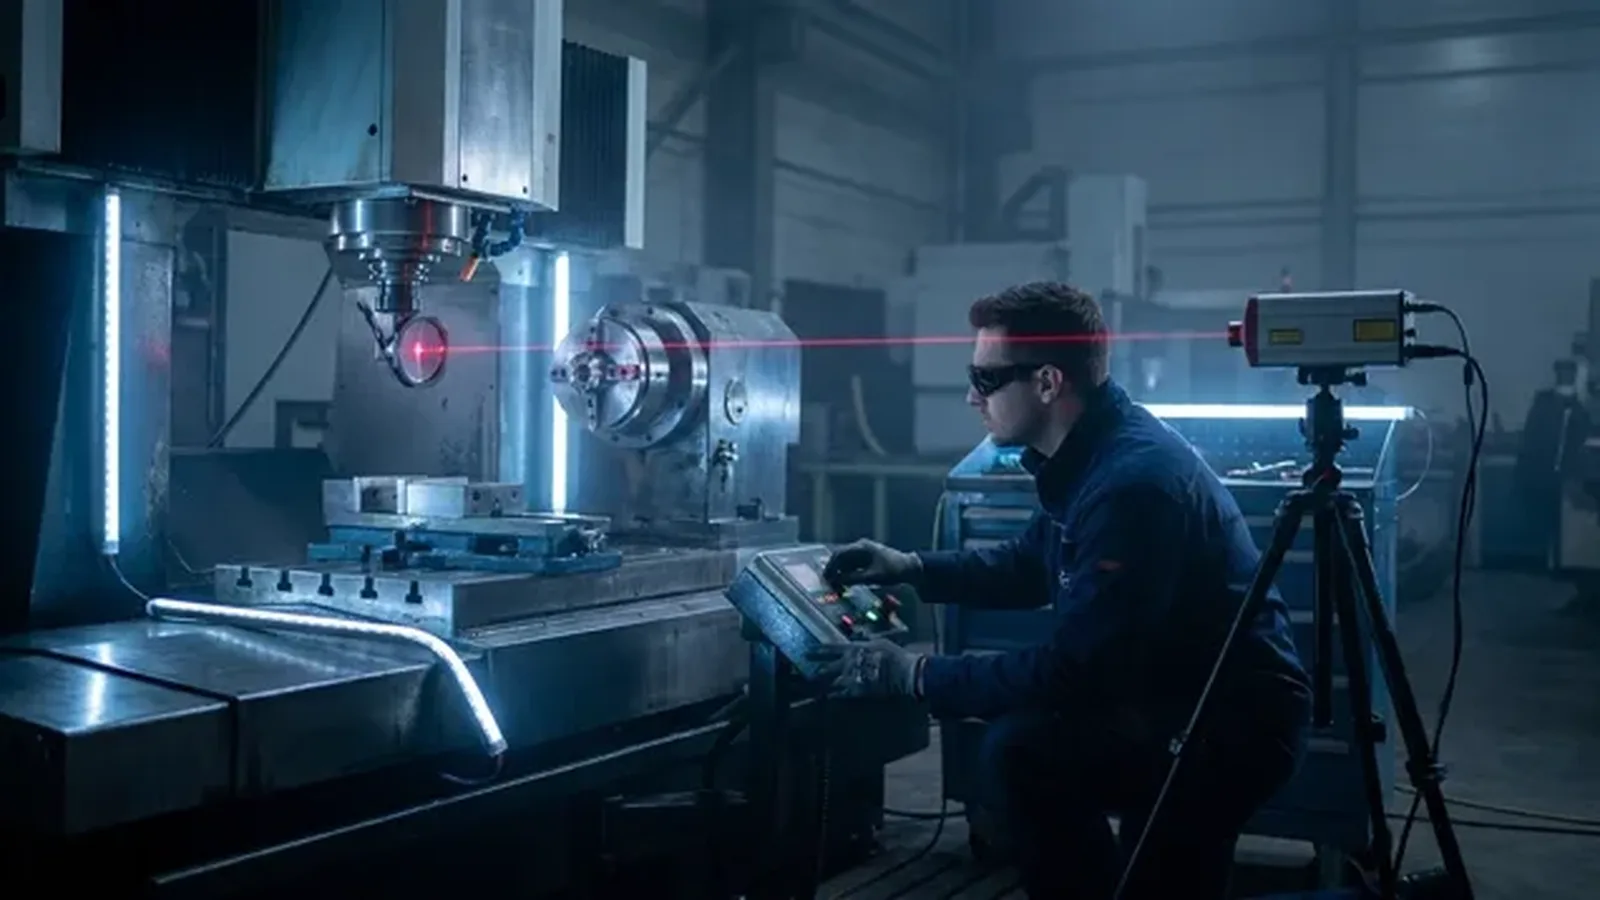
Fast diagnostics that catch circularity errors before scrap.
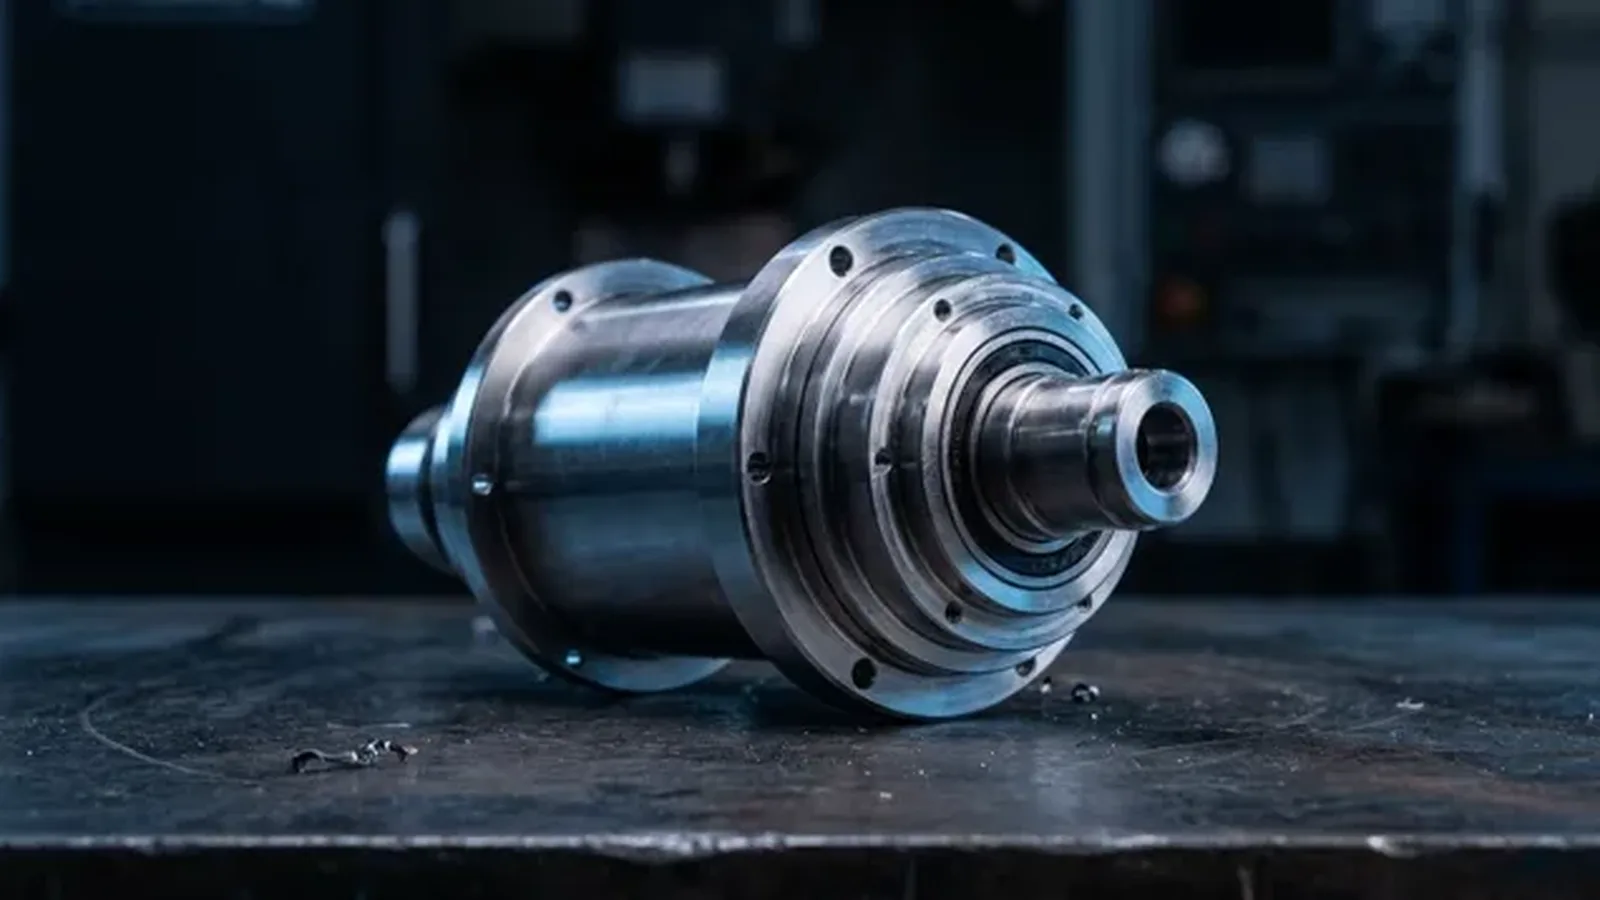
Diagnostic sequence for vibration, noise, heating, and surface deterioration.
WIESSER TURKEY TECHNOLOGY CENTER
Dilovası OSB 4th Section, Ceyhan Ave. No:29, Gebze / Kocaeli
0216 313 30 46 · WhatsApp 0534 694 13 85
The Art of Milling
We recommend the suitable machine type for your process based on material, tolerance, clamping method, and target quantity.